Same recipe, same machine — and the output still slips. It starts in the extruder. Screw, block, liner — they all wear, batch after batch. The gap grows, conveying weakens, mixing goes uneven — and one day the line stops. Twin-screw extruder wear checks exist to catch that drift early, while the fix is still a spare-parts order.
Why Regular Wear Inspections Are Essential for Powder Coating Plants
Maintaining Consistent Extrusion Performance
Factory sets the gap between screw and barrel tight — wear opens it. Conveying weakens. Output drifts. Every setting still reads the same.
Preventing Unexpected Downtime
Wear found early stays a scheduled job. Push it past early and it stops being a spare-parts order — it becomes a broken shaft and a line standing idle.
Controlling Maintenance Costs
Swap the worn part in a planned stop — the rest stays intact. Skip the checks, and damage compounds — small fixes become big repairs.
Key Components to Inspect for Wear in a Twin-Screw Extruder
Work the four wear points in the order below — that is what separates a real inspection from a glance.
Screw Segments and Screw Flights
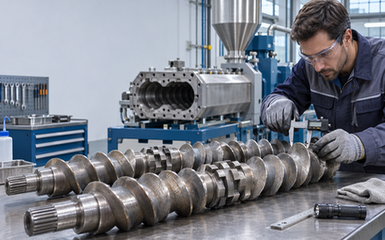
Each segment, scanned for scoring, pits, corrosion, uneven side wear. The flight edge is the tell — sharp means intact, rounded or thinned means material is gone. Measure the outside diameter too; conveying capacity follows that number down.
Kneading Blocks
Check block edges for wear, bending, or chipped corners, then see how neighboring blocks mesh. A thinned block stops filling the gap; the shear it creates weakens — color drift can trace back to blocks that still look fine.
Barrel Liners
Walk the inner wall — scratches, grooves, worn patches show up there. Inside diameter? Measure at several points, not one. Uneven wear shifts the clearance from spot to spot. Once screw-to-barrel clearance passes the maker’s limit, the liner is finished.
Screw Shafts and Drive Components
Couplings and splines first — fretting or play shows up there before anything else. Then check alignment; any unusual radial or axial movement. Gearbox, bearings, and lube system get the same pass — a troubled bearing usually announces itself through the oil first.
Common Warning Signs of Twin-Screw Extruder Wear
Reduced Production Output
The recipe is the same. The speed is the same. The feed is the same — and the line delivers less. Output slipping under unchanged parameters usually means screw or liner wear is eating the conveying capacity.
Unstable Torque and Motor Load
Torque that climbs, sags, or hunts — attention. Feed, temperature, raw material all move torque too. Check unstable extruder torque causes one by one before blaming wear.
Poor Mixing and Dispersion Quality
Pigment dispersion going uneven, color shifting batch to batch, quality wandering with no recipe change — worn screws or kneading blocks are the usual suspect. The twin-screw extruder dispersion review sorts mechanical causes from material ones.
Abnormal Noise and Vibration
Whine, knock, or new vibration? Check alignment, bearings, drive train — that is where it hides. Track it down promptly — noise is a cheap warning; a failed bearing is not.
How to Perform a Twin-Screw Extruder Wear Inspection
Run the check like a procedure, not a glance — work the steps in order.
Step 1 – Shut Down and Prepare the Equipment
Stop and isolate the machine per the maker’s procedure — power off, energy locked out. Let the barrel cool to a safe temperature, then stage gauges and camera.
Step 2 – Open and Clean the Extruder Barrel
Open the barrel per the manual. Residual melt? Clear it — it hides scratches. Work carefully around machined surfaces; a careless scraper does damage that later looks like wear.
Step 3 – Conduct a Visual Inspection
Go over screws, kneading blocks, and liners segment by segment. Photograph every mark, wear patch, or deformation and note where it sits — a spot near the feeding zone means something different from one at the discharge.
Step 4 – Measure Component Clearances
Gauge screw diameter, barrel diameter, clearances. Compare the readings — maker’s standard, machine’s history. Do not apply a universal wear limit — the maker’s number for this extruder counts.
Step 5 – Record and Evaluate Inspection Results
Log the wear location, values, photos. Monitor, repair, or replace — pick one. Dates on file make the next check a trend, not a guess.
How Often Should Powder Coating Plants Check Extruder Wear?
Hours, load, filler abrasiveness — they set the pace. Watch parameters, noise, and vibration daily — save the full internal inspection for planned stops. Run abrasive formulas or heavy load? Add checks in between.
Factors That Accelerate Twin-Screw Extruder Wear
Abrasive Raw Materials
Abrasive fillers and pigments work like sandpaper — every pass, screws and liners shed a little. More abrasive recipe, faster tolerance goes.
Improper Operating Conditions
Screw speed pushed too high, load run beyond the machine’s rating, or a layout that does not suit the material — each adds stress the parts were not built for.
Incorrect Assembly and Alignment
Shaft off-center? Clearance outside spec? Wear stops spreading — it stacks in one spot.
Inadequate Maintenance
Thin lubrication, stray foreign objects, rough cleaning habits — any one shortens component life. Follow the extruder lubrication routine — drive components stay off the wear list.
When Should You Repair or Replace Worn Extruder Components?
Surface wear inside the maker’s tolerance? Keep measuring and watch the trend — no shutdown needed. Cross the manufacturer’s allowable limit on screw diameter, block mesh, or barrel clearance and the part has used up its life — replace it. New segments, blocks, and liners need to match the originals: material, dimensions, mesh clearance, configuration — and assembly follows the maker’s specs. Why so exact? Because a close-enough fit wears out its neighbor.
How MPMtek Twin-Screw Extruders Support Long-Term Reliability
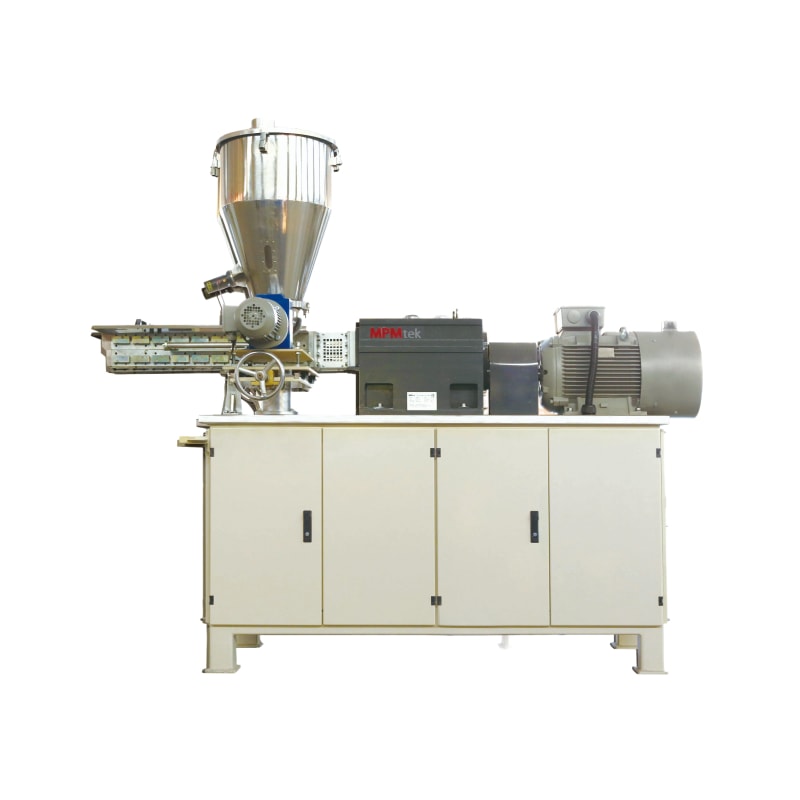
MPMtek twin-screw extruders: alloy steel, heat treatment, precision machining — built for less-urgent checks. The screws, blocks, and liners hold mesh clearance for the machine’s life — mixing stays stable, and the screws self-wipe as they turn. Capacity and screw configuration match the formulas a plant actually runs. Sizing the next machine? The MPMtek twin screw extruder specifications are the place to start.
Conclusion: Keep Your Powder Coating Extruder Running Reliably
Checks on schedule, records honest — performance, quality, and the production calendar all hold. Sizing a new line? Send MPMtek your hours, wear data, target output — then pick the extruder that fits.
Frequently Asked Questions
How often should twin-screw extruder screws be inspected?
Start from the manufacturer’s advice. Then adjust — hours, load, abrasiveness. Heavier load, more abrasive recipe — shorter interval.
What are the common signs of extruder screw wear?
Falling output at unchanged settings, visible surface wear, drifting mix quality, torque moving for no process reason.
When should twin-screw extruder components be replaced?
Once key dimensions or clearances step outside the manufacturer’s allowable range — or the damage starts affecting machine performance — replace the component.